
In a liquid-cooled battery pack, the weld is one key control point for sealing integrity and manufacturing reliability. It sits alongside the other things that decide cooling performance: channel geometry, the TIM and contact interface, the coolant loop, and how the finished plate is validated. A cold plate carries heat from the cells into a flowing coolant, and that heat path only works if the joint between cover and base stays sealed and conducts heat across the interface. This article covers how liquid cold plates are joined: friction stir welding, vacuum brazing, and gas-shielded welding. It also explains why aluminum is both the obvious and the awkward material for the job, and how weld quality is verified before a plate ships. The scope stays inside the cell-to-coolant thermal path and does not cover cell chemistry, BMS control, or vehicle-level energy strategy.
Challenges of Liquid Cold Plates in Battery Packs
Three constraints shape a liquid cold plate before it reaches a pack: design coupling, manufacturing precision, and in-service leak risk. Each one maps to a decision an engineer makes before the plate is joined, not after.
Design has to reconcile fluid dynamics, heat transfer, and structural layout together. A channel pattern that looks efficient on a thermal map can raise pressure drop enough to force a larger pump or starve the hottest cells of flow. Flow resistance and temperature uniformity therefore have to be validated as one problem, because fixing one after the fact usually disturbs the other.
Manufacturing precision and cost pull in opposite directions. Tight channel tolerances and high-purity aluminum raise machining time and scrap risk. The joining process chosen at this stage sets much of the per-unit cost and the leak behavior for the life of the plate.
Leak risk carries more weight here than in a general heat exchanger. A liquid loop inside a live battery pack means any coolant leak is a safety event, so joint integrity and pressure testing sit near the top of the acceptance list. Cooling stability itself depends on flow rate, pressure drop, and inlet temperature staying inside their design window, which is why a pack needs monitoring instead of a set-and-forget assumption.
Where Liquid Cold Plates Are Used
Application duty, not preference, decides which cold plate construction fits. The four groups below share a cooling principle but differ in heat flux, pressure, and packaging.
- Power battery packs. Cold plates manage the heat of high-capacity cells in EVs, holding cell temperature and pack uniformity across charge, discharge, and fast-charge loads.
- Energy-storage packs. In stationary systems, plates keep cells near their optimal band so the array stays safe and efficient over long cycling; this is central to battery energy storage systems tied to renewables and the grid.
- High-heat-flux power electronics. Inverter and IGBT heat exchangers, plus photovoltaic power-conversion cooling, use cold plates where component heat flux is concentrated.
- Process-cooling components. Freeze-dryer and chiller heat-exchange parts use liquid cold plates where precise temperature control matters.
Construction usually falls into a few families, and the split matters because the joining method follows from it. Vacuum-brazed plates suit complex internal fin geometries; friction-stir-welded plates suit machined or extruded channels where joint strength governs; exposed-tube plates route coolant tubes pressed into or bonded to the plate body for a simpler build; and drilled-passage plates run long gun-drilled holes through solid aluminum or copper. Cost and reliability are not fixed labels on these families. They follow from structure, material, sealing, and production conditions. Choosing among the different types of cooling plates is really a choice about how the coolant path will be formed and sealed.
Why Aluminum — and What Makes It Harder to Weld
Aluminum earns its place in cold plates on conductivity-to-weight and formability, not on raw conductivity. Its thermal conductivity is several times that of stainless steel, which lets an aluminum plate shed heat efficiently. Copper still conducts more heat per unit volume; aluminum wins on conductivity per unit mass and on how easily it machines and forms into intricate channels. In a pack, that lighter plate helps the thermal and structural integration budget, and the material choice stops there. It does not translate into a vehicle-range claim.
The properties that make aluminum easy to shape make it harder to weld cleanly. Three effects drive most of the difficulty:
- Low melting point and high heat conduction spread the heat-affected zone. In fusion welding, they invite porosity and cracking as the weld pool solidifies.
- A tenacious oxide film forms almost instantly on the surface. Aluminum oxide melts far higher than the base metal, so it must be removed before joining or it becomes trapped in the weld.
- A high coefficient of thermal expansion produces more distortion during welding, so a thin cover needs fixturing and process control to hold flatness.
All three constraints are manageable, and manufacturers choose the joining process partly to work around them. Surface preparation, fixturing, and solid-state joining all exist to keep aluminum’s advantages while controlling how it behaves when heated.
Joining Processes: FSW, Vacuum Brazing, and Gas-Shielded
No single joining method wins for every cold plate; volume, pressure duty, channel complexity, alloy, and leak tolerance decide. It also helps to keep the categories straight: friction stir welding and gas-shielded welding join the metal itself, while vacuum brazing bonds parts with a separate filler alloy.
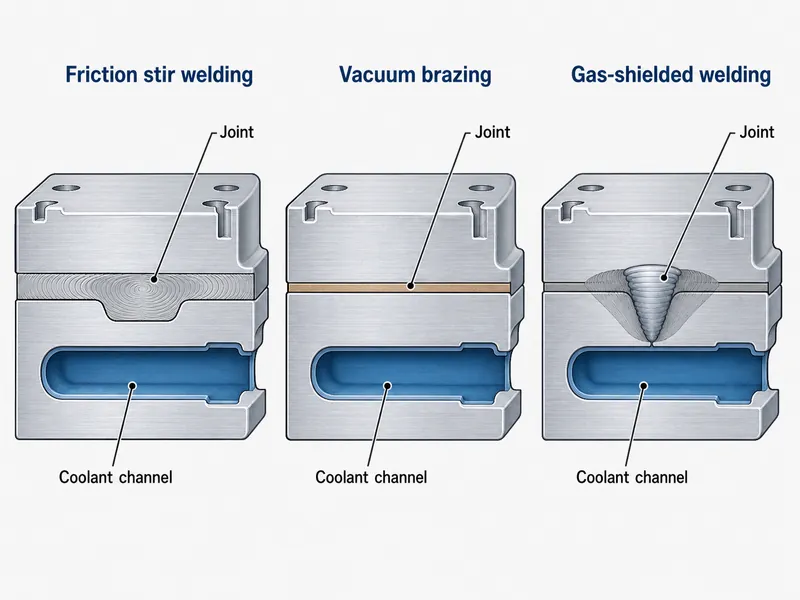
Friction stir welding (FSW) is a solid-state process. A rotating tool stirs the aluminum into a joint without melting it. As NASA notes, friction stir welding joins aluminum alloys that are difficult to fuse-weld and produces high-strength, virtually defect-free joints. The Welding Institute invented and patented the technique in 1991, and NASA later used it on aluminum tanks for launch vehicles. Because the metal never liquefies, FSW largely avoids the porosity and solidification cracking that trouble fusion welds. It suits machined or extruded plates and repeatable runs, though it needs rigid fixturing, accessible weld lines, and its own control of lack-of-penetration and root or interface defects.
Vacuum brazing joins the plates with a filler alloy that melts below the base aluminum. Capillary action draws the filler into the joint inside a vacuum furnace. Its strength is complex internal geometry: brazing can bond dense folded or offset-strip fins across a large surface area in one furnace cycle. The trade-offs are furnace capital cost, longer cycle times, and joint conductivity limited by the filler alloy.
Gas-shielded welding is an arc fusion process performed under a shielding gas. It is comparatively low-cost and gives good pressure resistance, but it adds filler and heat input, which raises distortion and often means added process control or post-weld treatment.
| Process | Category | Typical fit | Main trade-off |
|---|---|---|---|
| Friction stir welding | Solid-state welding | Machined/extruded channels, repeatable volume | Rigid fixturing; accessible weld lines; control of unwelded roots |
| Vacuum brazing | Brazing (filler alloy) | Complex internal fins, high surface-area density | Furnace cost and cycle time; conductivity set by filler |
| Gas-shielded welding | Arc fusion welding | Lower-cost builds needing pressure resistance | Higher heat input and distortion; filler and rework |
Process control differs by method, so there is no single parameter set. FSW is governed by tool rotation, travel speed, downforce, and fixturing; vacuum brazing by furnace temperature, vacuum level, and filler selection; gas-shielded welding by heat input, filler, and shielding gas. Cost follows the same branching logic. Furnace-based brazing carries equipment and cycle-time cost that pays off on complex, high-mix work, while stir welding shifts cost toward tooling that pays off on repeatable plate designs. Where cold plate manufacturers report figures for joint strength, pressure, or cycle time, treat them as vendor data tied to a specific plate and process, not as general constants.
How Weld Defects Undermine Cold Plate Performance
A joint that fails inspection threatens two things separately: the seal and the heat path. Keeping them separate explains why later inspection is not optional.
Weak or incomplete joints are a leak and structural problem first. Low joint strength invites cracking and coolant leakage, which inside a battery pack compromises structural integrity and can escalate into a thermal event. Distortion and grain growth are a dimensional problem: warping a thin cover breaks the flatness that even contact with the cells and the thermal interface depends on, so uneven cooling and hot spots can follow. A joint with poor contact or trapped defects can also raise thermal resistance across the interface it sits on, which matters most where that joint lies in the conduction path. These effects are why manufacturers hold joining parameters inside qualified windows. Where a process uses filler and shielding gas, they match it to the alloy instead of choosing by habit.
Inspecting Cold Plate Welds: NDT Methods
Non-destructive testing checks a production plate’s surface, near-surface, and internal joints without cutting it apart. It complements process qualification and pressure or leak testing; it does not replace them, and not every critical defect is internal. The method is chosen for the defect being hunted, and more than one is often combined on the same plate.
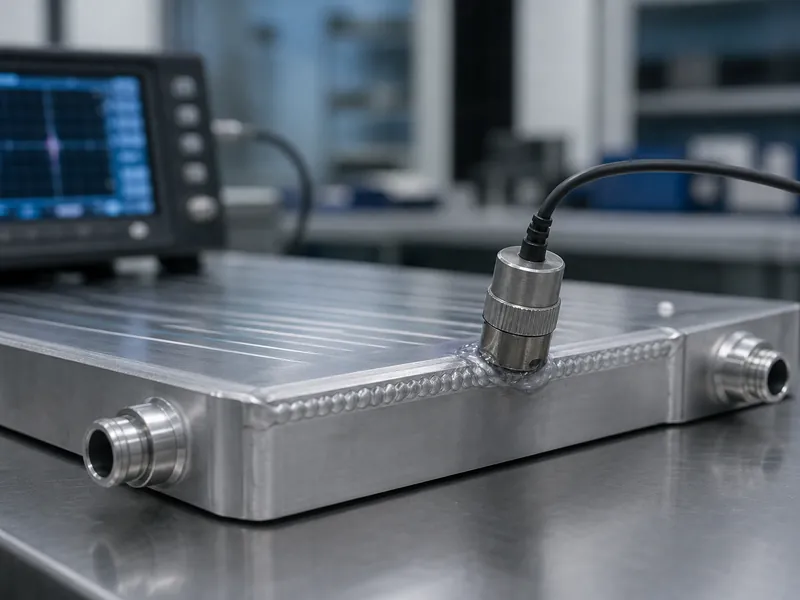
- Visual inspection judges surface integrity, uniformity, visible cracks, and porosity; it is the first pass and cannot see inside the joint.
- Radiographic testing (RT) uses X-ray or gamma energy to reveal internal porosity, inclusions, and cracks, and it leaves a permanent image record, useful for complex geometry though slower.
- Ultrasonic testing (UT) sends high-frequency sound into the joint and reads the echoes from internal flaws; it suits thicker sections and single-sided access.
- Liquid penetrant testing (PT) draws dye into surface-breaking defects and suits non-magnetic aluminum.
- Eddy current testing finds near-surface defects through induced currents.
One caution is specific to aluminum: magnetic particle inspection relies on a ferromagnetic material, so it does not apply to aluminum cold plates the way it does to steel welds, and penetrant or volumetric methods take its place. Trumonytechs inspects the weld seam after each weld and selects the method, or a combination, to match the joint and geometry in front of the inspector. Pressure and leak testing then confirm the sealed loop holds under service conditions before the plate reaches a pack.
Weighing Cold Plate Joining Options for Your Pack
Start the joining decision from the plate’s channel design and its leak tolerance, then screen processes against alloy, thickness, weld-line access, production volume, and how the joint will be inspected. A machined or extruded plate that cannot tolerate leakage often points toward a solid-state joint, provided the weld lines are reachable and roots can be verified. A plate that depends on dense internal fins points toward brazing, because a furnace braze can form geometry a stir tool cannot, with the filler-limited conductivity accepted as part of the trade. Where cost dominates and pressure duty is moderate, gas-shielded welding can be the pragmatic answer once distortion and rework are planned in.
Whatever the process, the joint has to be verified, not assumed. Internal porosity and incomplete fusion stay invisible on the surface, and on aluminum the inspection method has to fit a non-magnetic material. Getting the joint and its acceptance right is what lets an aluminum cold plate do its real job in battery thermal management: moving heat out of the cells within qualified sealing, pressure, and defect limits. Trumonytechs matches the joining and inspection approach to the plate design and duty when supplying liquid-cooled plates for EV and ESS packs.
FAQ
Is friction stir welding or vacuum brazing better for a battery cold plate?
Neither is universally better; channel design and leak tolerance decide. FSW is a solid-state joint that avoids fusion porosity and suits machined or extruded channels, while vacuum brazing is chosen when the plate needs dense internal fins a furnace braze can form. One limit remains: a solid-state joint still needs its roots and weld-line access verified, so accessibility can rule it out even when leak tolerance favors it.
Why is aluminum used for cold plates if it is harder to weld?
Aluminum is used because its conductivity-to-weight ratio and formability outweigh its welding difficulty. It conducts heat several times better than stainless steel and machines easily into intricate channels. The low melting point, oxide film, and distortion that complicate welding are handled through surface preparation, fixturing, and often solid-state joining.
How do you check a cold plate weld for internal porosity without cutting it open?
Volumetric non-destructive methods find internal porosity, mainly radiographic and ultrasonic testing. Radiography images internal pores, inclusions, and cracks, while ultrasonic testing reads echoes from internal flaws and works with single-sided access. Visual and penetrant testing catch surface defects separately, and none of these replaces a pressure or leak test of the finished loop.
Does magnetic particle inspection work on aluminum cold plates?
No. Magnetic particle inspection needs a ferromagnetic material, and aluminum is non-magnetic. Inspectors check aluminum joints with liquid penetrant testing for surface defects, and radiographic or ultrasonic testing for internal ones.
Which joining process fits high-volume EV pack production?
For repeatable machined or extruded plates in higher volumes, friction stir welding often fits, because its solid-state joint is consistent and its cost sits mostly in tooling and fixturing. Vacuum brazing stays preferable when each plate needs complex internal fin structures, whatever the volume; the deciding factor is geometry, not throughput alone.
Further Reading
- NASA — Friction Stir Welding — Government (T1). Supports the point that FSW is a solid-state process that avoids the melting-related porosity and distortion seen in fusion welding of aluminum.
- NASA — Friction Stir Weld — Government (T1). Supports that FSW joins aluminum alloys difficult to fuse-weld and produces high-strength, near-defect-free joints, and attributes the process to The Welding Institute (1991).
Related Articles
- Battery Liquid Cooling System Overview — Traces why passive air cooling gave way to liquid cold plates as battery thermal loads rose.
- Avoiding Corrosion in Liquid Cooling Systems — Explains coolant chemistry and inhibitors that keep cold plate loops from corroding in service.
- Liquid To Air Heat Exchanger: Boost EV Cooling & Life — Shows how the coolant loop rejects battery heat to air downstream of the cold plate.
- Overcoming Thermal Management Challenges In The Electric Vehicle Industry: Comprehensive Guide — Sets the pack-level temperature targets that cold plate cooling is designed to hold.
- Why Electric Vehicles Need Lithium-Ion Batteries for Charging and Discharging? — Background on the cells whose heat the cold plate has to carry away.
